
Operating a Split-Type Roughness Tester: Five Key Points
With probe and body separated, five details decide whether the data holds up: how the probe sits, which way it travels, where you measure, what parameters you set, and who is driving.
1. Let the probe settle – do not press
The probe rests on the surface under its own weight or a constant spring load. Pressing it shifts the stylus relative to the workpiece and biases the reading high; holding it too loosely lets the stylus skip between peaks and valleys, and the number swings. Put it down vertically, let it settle, then drive it horizontally at constant speed without adding force.
2. Measure across the lay
Turning, milling and grinding all leave a directional texture. The measurement direction should be perpendicular to the lay, so the stylus crosses real peaks and valleys; run it along the lay and the stylus stays in one groove, and the value comes out low. When the drawing says nothing about direction, three measurements across the lay, averaged, is the safe convention.
3. Stay away from edges, holes and damage
Roughness is not uniform across a part. Edges, bore mouths, recesses and scratches are not representative, and a number taken there means nothing. Choose an area where the machining texture is even and the surface flat.
4. Match the cutoff to the process
Too short a cutoff misses the real roughness; too long pulls waviness into the result. Normal machined surfaces take 0.8 mm, coarser surfaces 2.5 mm, and the evaluation length is normally five cutoffs. Before comparing readings from two instruments, confirm both use the same cutoff and evaluation length – otherwise the same surface will disagree by a visible margin.
5. Know what you are measuring
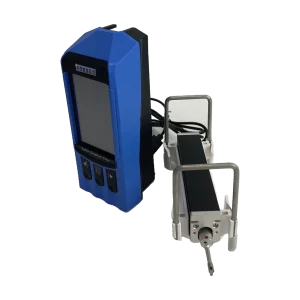
The operator should be able to tell Ra from Rz, know which filter the instrument is applying, and judge whether an odd reading comes from the surface or from the instrument. On a split-type unit the probe is a separate part: knocks and cable strain degrade accuracy quietly, so clean it after use and store it on its own.
Summary
The value of a separate probe is access. Whether the number is right depends on the five points above – probe seated, direction correct, parameters consistent. Those three matter more than the price of the instrument.
Related products
Tell us the workpiece, thickness range and accuracy you need — we will reply within 8 hours.

